Busbar Fabrication Equipment for Nigerian Switchgear, Panel and Busduct Manufacturers
2026-11-10
Topic: Nigerian switchgear busbar fabrication · equipment configuration · 3-in-1 vs CNC
Brand focus: LTMC 303U-3-C · 503U-3-C · 803U-3-C
For: Switchgear, panel and busduct shops in Lagos, Abuja, Port Harcourt and Kano · three-phase 415 V / 50 Hz
Quick answer
Choose busbar fabrication equipment for a Nigerian switchgear, panel or busduct shop from approved drawings, material grade and temper, width × thickness, hole and slot layout, bend geometry, tolerances, batch mix and conforming output — not nominal force alone. A hydraulic 3-in-1 (LTMC 303U-3-C / 503U-3-C / 803U-3-C) suits mixed or lower-volume panels in Lagos, Abuja, Port Harcourt or Kano. Servo or CNC positioning helps recurring hole and length kits; dedicated punch–shear lines or bend centres fit high parallel load. Confirm punch, shear, flat-bend and edge-bend capacity separately, then prove the package with samples and FAT before shipment to Lagos.
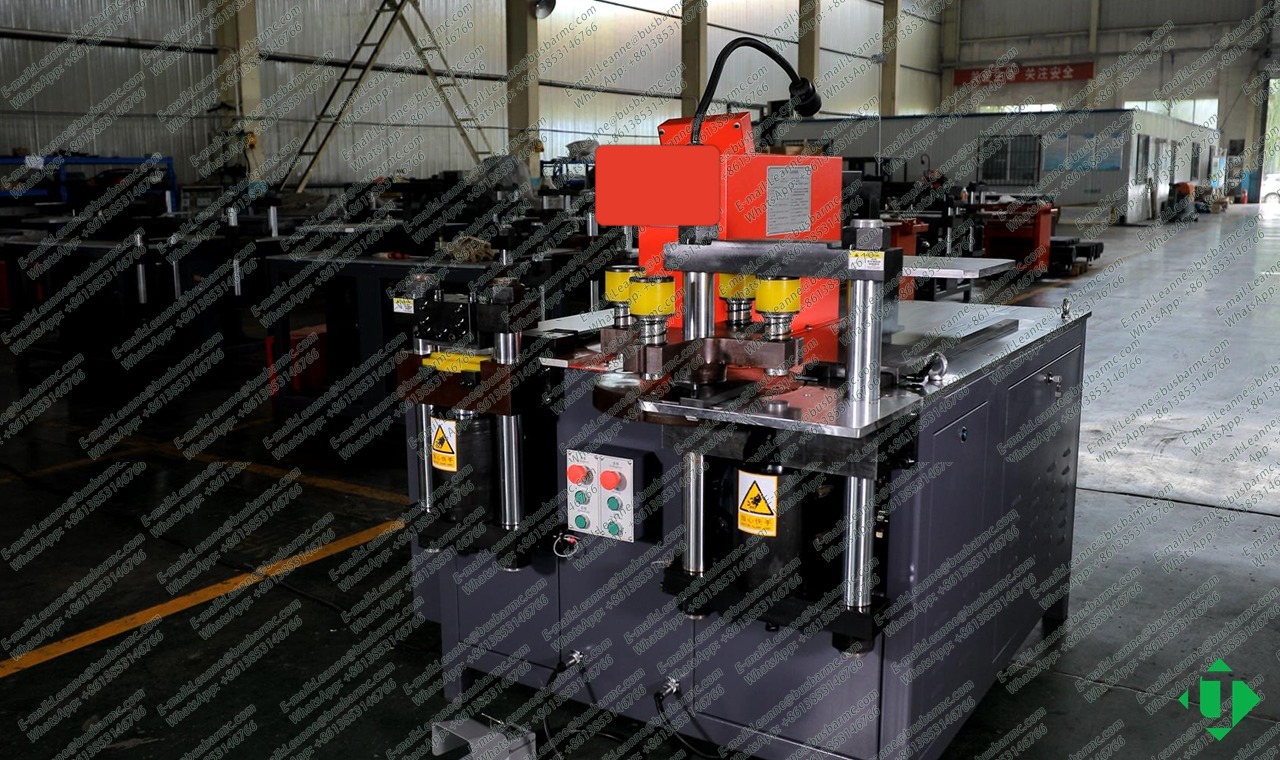
LTMC factory view of a multi-station busbar machine
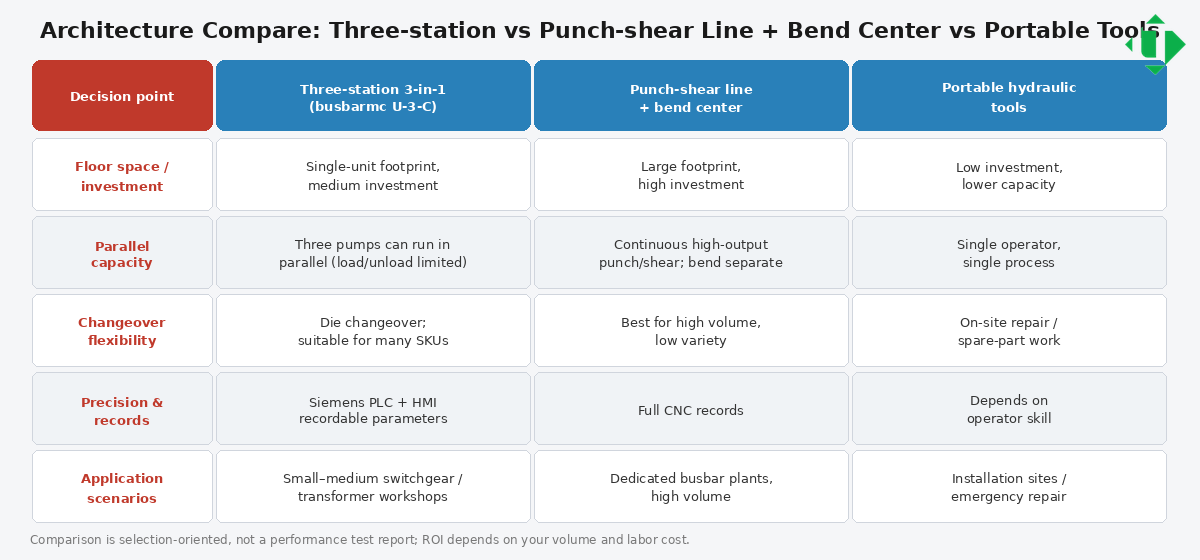
Architecture compare: 3-in-1 vs dedicated vs portable
Operations required for switchgear busbars
| Operation | Finished-part need | Equipment check |
|---|---|---|
| Cut / shear | Length, square, burr | Blade + capacity |
| Punch / slot | Size, pitch, edge distance | Die list + positioning |
| Flat bend | Released angle, radius, short leg | Springback + tooling |
| Edge / vertical bend | Direction + tighter envelope | Separate capacity |
| Complex multi-bend | Assembly envelope | Sequence + interference |
| Mark / deburr / inspect | Traceability + safe edges | Included vs separate |
| Handling | Long/heavy bars | Rollers, crane, staff |
The machine fabricates geometry. It does not by itself set current rating, phase spacing, or clearance rules—those stay with the switchgear design.
Configuration map for switchgear shops
| Production pattern | Starting configuration | Critical buyer check |
|---|---|---|
| Custom panels, lower volume | Hydraulic 3-in-1 or separate hydraulics | Per-station capacity + tooling |
| Mixed recurring models | Servo / HMI recipe 3-in-1 | Program recall + remaining manual steps |
| Repeated holes & fixed lengths | CNC punch–shear line | Feed travel, dead zone, nesting |
| Complex / bottleneck bending | Dedicated programmable bender | Short leg, springback, clearance |
| High parallel workload | Separate punch / cut / bend | Queue time + staffing |
| Wide / thick / long bars | Heavy class + external support | Max-size test on FAT |
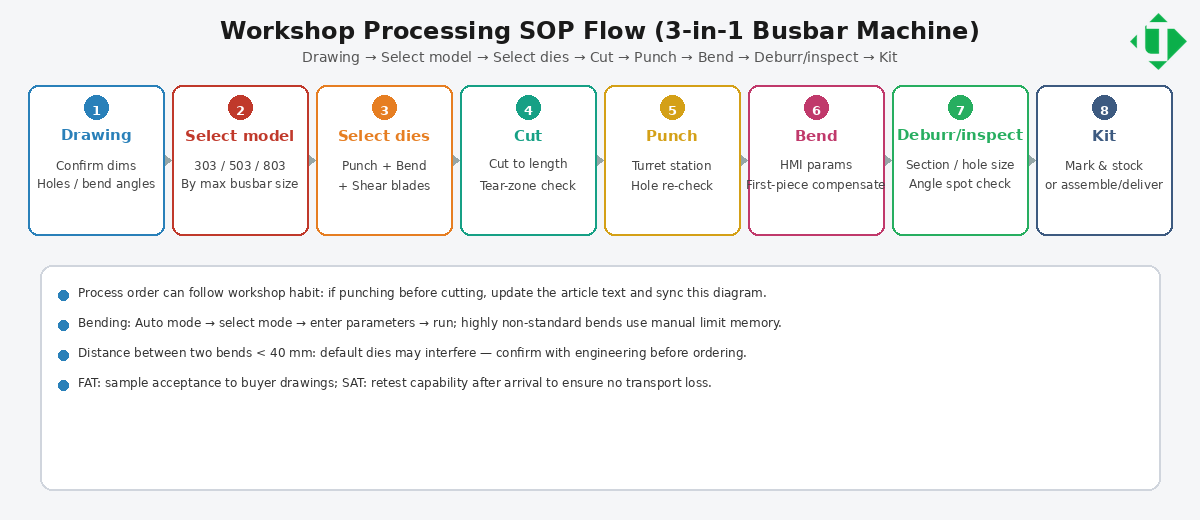
Workshop SOP flow: Drawing → Cut → Punch → Bend → Inspect
Why LTMC 3-in-1 fits many panel builders
One frame hosts punch turret, shear, and bend with three pump groups for sequential or parallel staffing—compact footprint for SME switchgear cells.
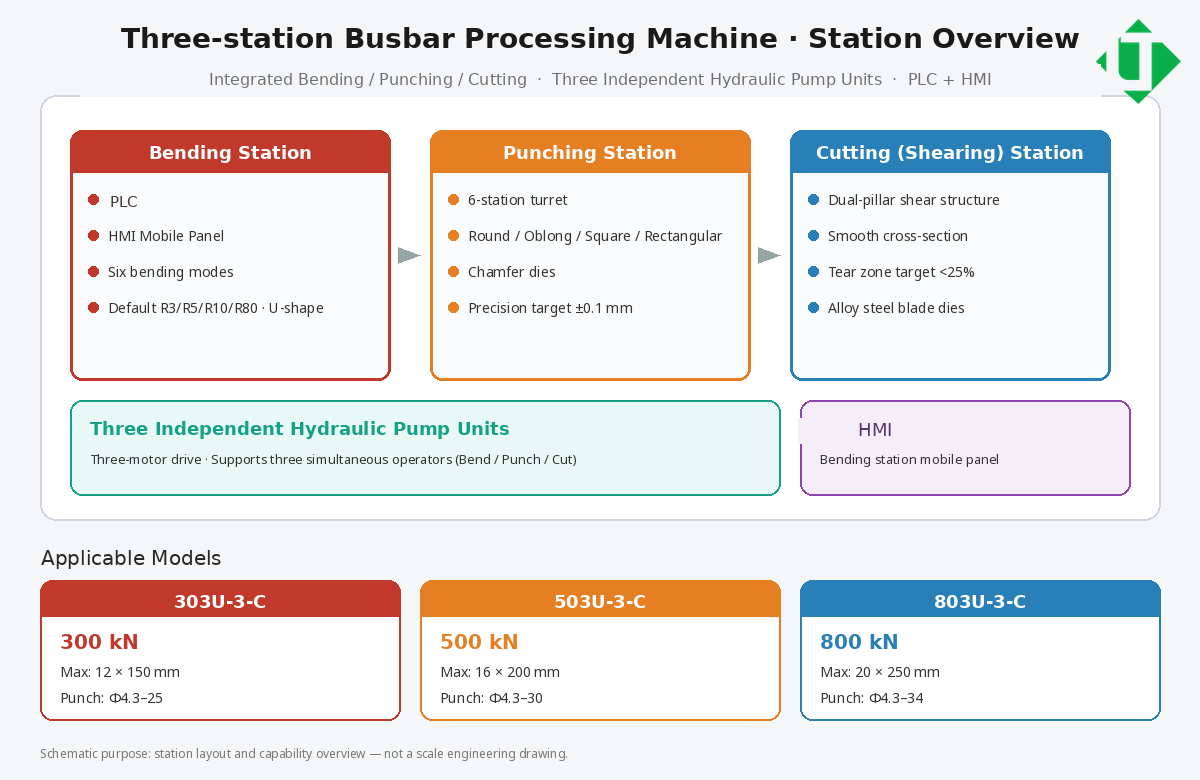
Three-station layout overview with English callouts
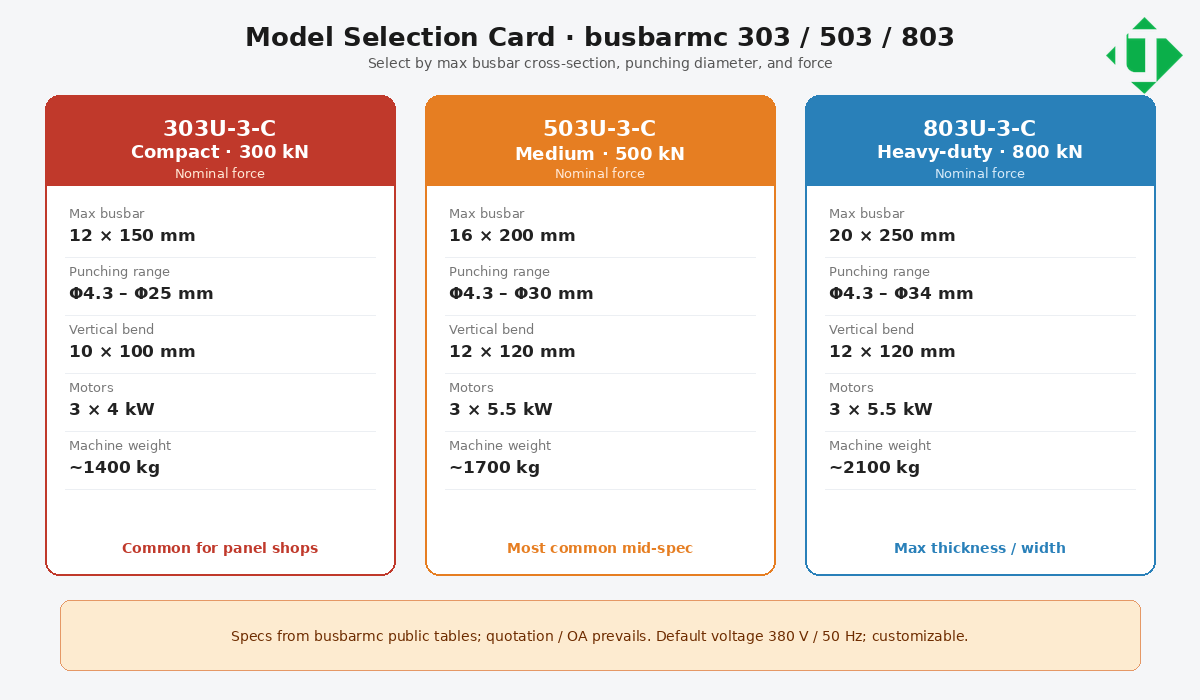
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
| Entity | 303U-3-C | 503U-3-C | 803U-3-C |
|---|---|---|---|
| Nominal force (kN) | 300 | 500 | 800 |
| Punching diameter (mm) | Φ4.3–Φ25 | Φ4.3–Φ30 | Φ4.3–Φ34 |
| Max thickness / width (mm) | 12 / 150 | 16 / 200 | 20 / 250 |
| Max horizontal bend (mm) | 150 / 12 | 200 / 16 | 250 / 20 |
| Max vertical bend size (mm) | 10×100 | 12×120 | 12×120 |
| Motor power | 3×4 kW | 3×5.5 kW | 3×5.5 kW |
Selection & FAT for switchgear RFQs
- Send representative cabinet busbar drawings (holes, bends, lengths).
- State Cu/Al, temper, max section, monthly mix.
- List must-hit tolerances and inspection instruments.
- Agree FAT sample set (first / middle / last of a short run).
- Confirm voltage (typically 415 V / 50 Hz for Nigerian workshops; confirm the nameplate at order) and HMI language.
FAQ
What equipment does switchgear busbar work need?
Typically cut, punch, bend, deburr, mark, and inspect—plus handling for long bars.
Is a 3-in-1 enough for switchgear?
Often yes for mixed SME work. Scale to dedicated or CNC lines when volume or parallel load outgrows one frame.
Flat vs edge bend in cabinets?
Both appear in switchgear. Edge/vertical capacity is usually tighter—verify separately.
Does the machine set electrical clearances?
No. It produces mechanical geometry; electrical design stays with the approved arrangement.
Related technical guides
- 3-in-1 Busbar Processing Machine for Nigerian Panel Builders — Punch, Cut and Bend in One Frame
- How to Choose a Copper Busbar Machine for a Nigerian Panel Shop — Punch, Cut and Bend
- How CNC Busbar Machines Improve Output in Nigerian Switchgear Workshops
- What Is a Busbar Machine? Cutting, Punching and Bending for Nigerian Switchgear Work
Talk to LTMC about a machine for a Nigerian workshop
If you are specifying a punch, cut and bend package for a switchgear, panel or busduct shop in Lagos, Abuja, Port Harcourt or Kano, tell us the copper or aluminium sizes you run, the daily piece count, and whether the machine will sit on a three-phase 415 V / 50 Hz supply. Lighting circuits at 230 V / 50 Hz are not suitable for these machines.
Sea freight is normally arranged to Apapa, Tin Can Island or Lekki Deep Sea Port in Lagos, with Form M and SONCAP documents prepared against the commercial invoice. Leanne will confirm voltage, dies and packing before the machine leaves the factory.
Email [email protected] or WhatsApp +86 13853146766. You can also use the contact form on this site. Public model pages: 3-in-1 busbar machines, 303U-3-C, 503U-3-C, 803U-3-C, plus CNC bending, CNC punching and cutting, and dies and moulds.