How to Choose a Copper Busbar Machine for a Nigerian Panel Shop — Punch, Cut and Bend
2026-11-10
Topic: Copper busbar machine selection for Nigerian panel shops · process route · tooling · FAT
Brand focus: LTMC 303U-3-C · 503U-3-C · 803U-3-C
For: Switchgear, panel and busduct shops in Lagos, Abuja, Port Harcourt and Kano · three-phase 415 V / 50 Hz
Quick answer
A copper busbar machine for a Nigerian panel shop may be one integrated 3-in-1 (LTMC 303U-3-C / 503U-3-C / 803U-3-C) or a set of dedicated punch, shear and bend stations. Start from the approved finished-part drawing: material temper, datums, holes and slots, finished length, bend lines, radii, short legs and assembly interfaces. Confirm punching, shearing and bending capacity separately — catalogue maximum size does not prove every operation on every geometry. Compare routes by complete cycle time, tooling, handling, first-article yield and FAT evidence, and state a three-phase 415 V / 50 Hz supply when you request a quotation.
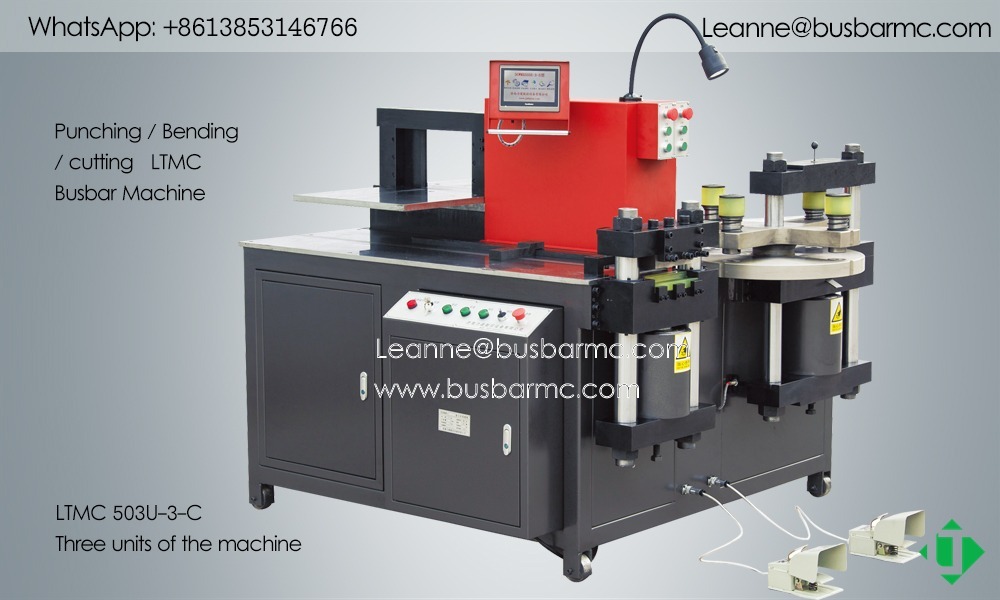
LTMC 503U-3-C three-station busbar machine overview
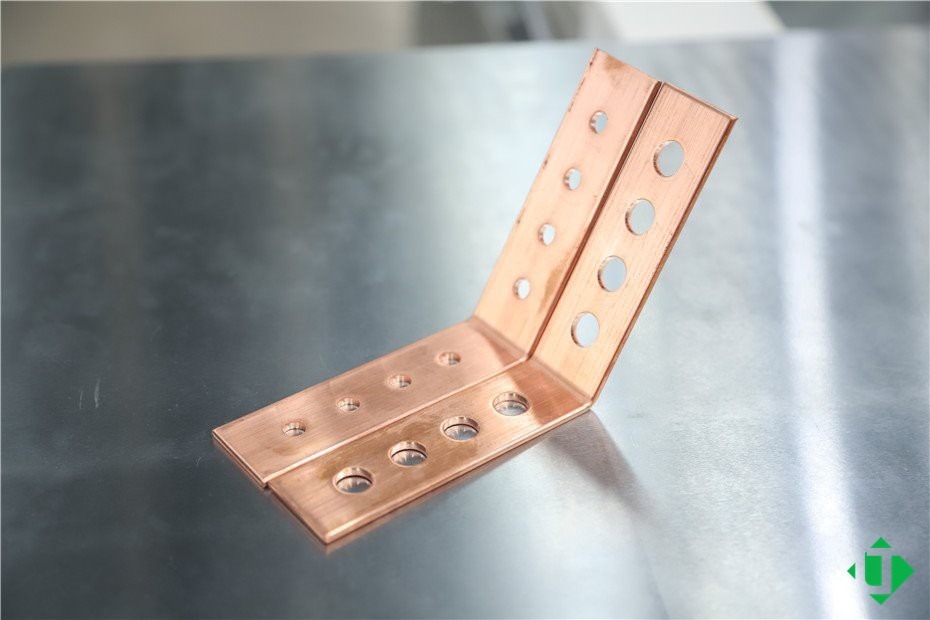
Copper samples after cut, punch and L-bend
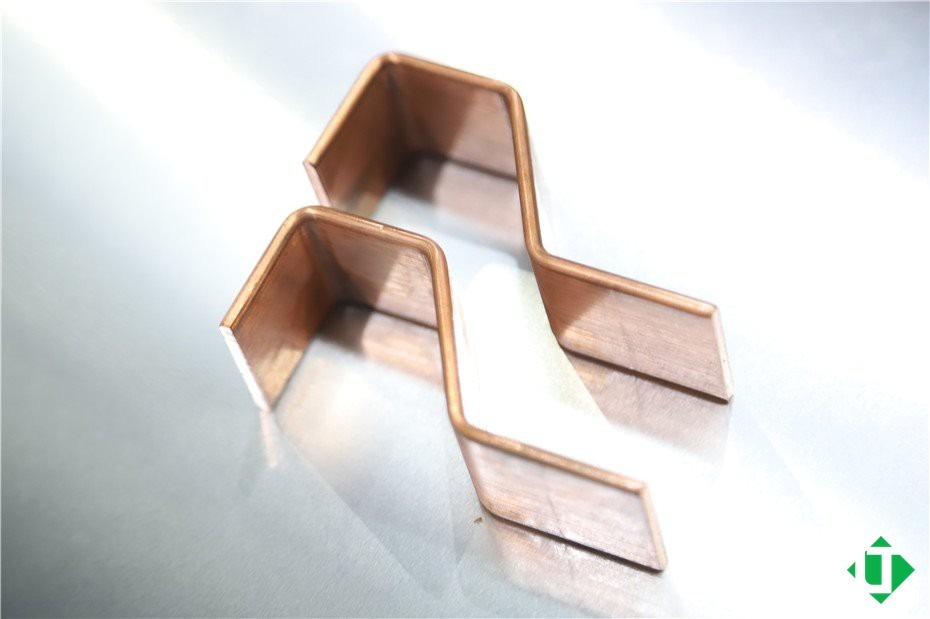
Copper Z / offset bend samples
Copper applications that drive machine choice
| Application | What to review |
|---|---|
| Switchgear & panels | Hole layout, bend structure, cabinet clearances |
| Transformer connections | Section, terminal holes, surface, interface |
| Busduct / long runs | Length support, joints, volume |
| Energy storage / charging | Dense holes, compact bends, surface control |
Select from the finished-part family, not the application name alone.
Process route options
| Route | Best fit | Trade-off |
|---|---|---|
| Hydraulic 3-in-1 | Mixed copper kits, limited floor | Manual transfer between stations |
| CNC / servo-assisted 3-in-1 | Recurring copper drawings | Still one-frame capacity ceiling |
| Dedicated punch / shear / bend | High hours per process | More footprint |
| Automatic CNC line | High volume nesting | CapEx + floor |
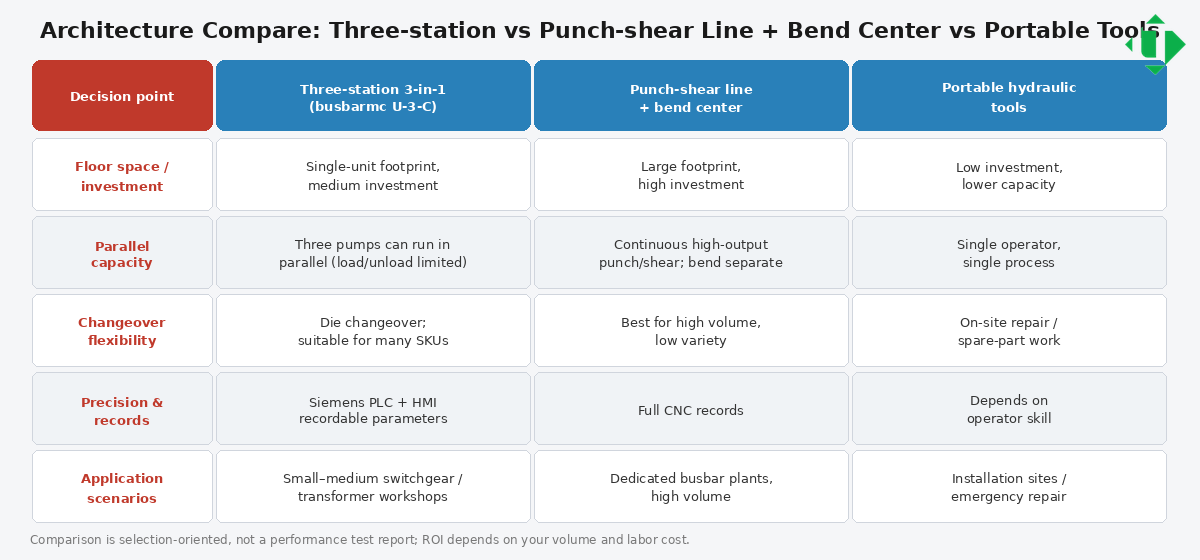
Architecture compare: 3-in-1 vs dedicated vs portable
Tooling that actually defines copper capability
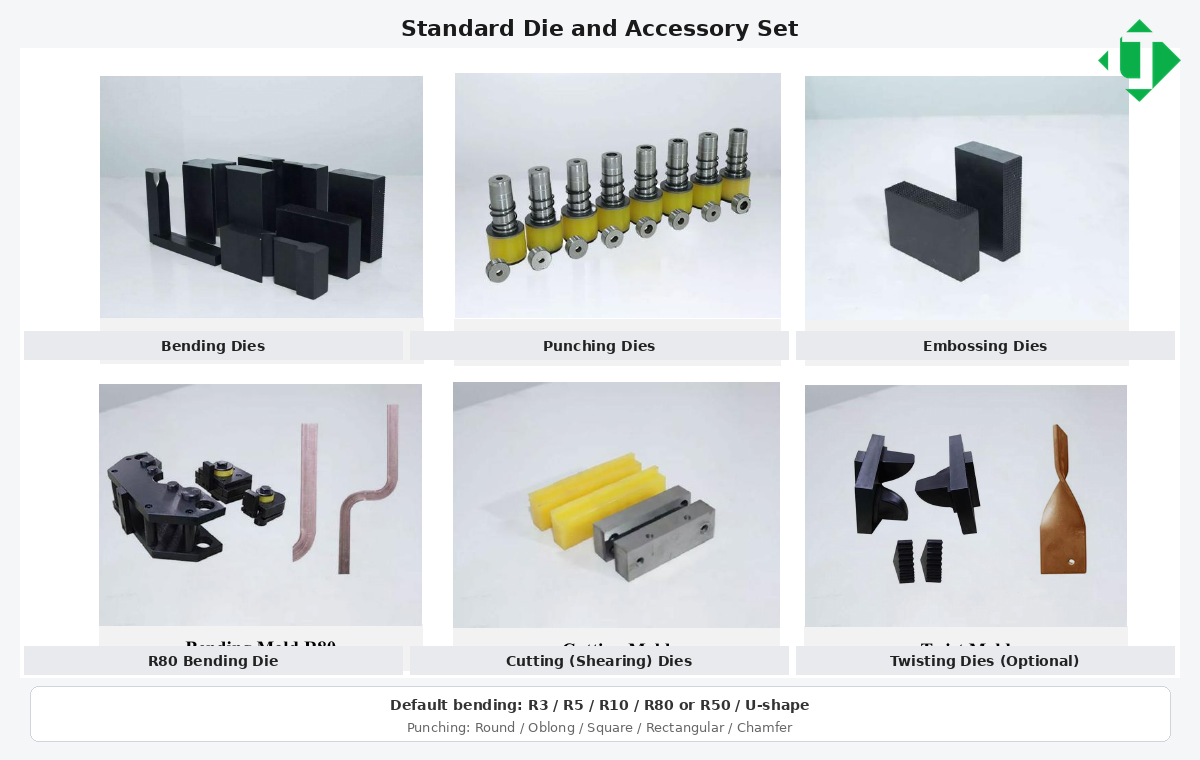
Standard die and accessory set with English labels
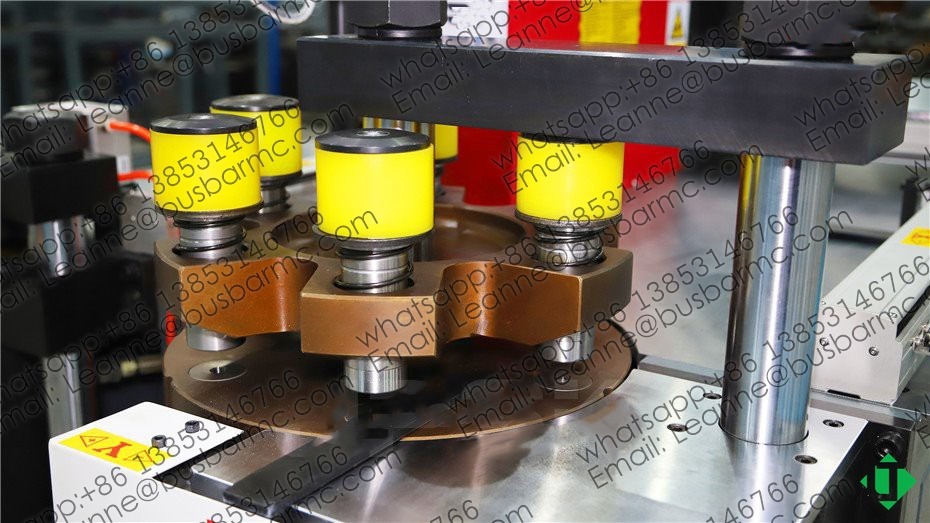
Punching turret unit with multi-station dies
- Punch: round / oblong families; published ranges Φ4.3–25/30/34 by model
- Shear: blades + clearance for copper temper
- Bend: R3/R5/R10/R80 (or R50), U-dies; flat vs edge modes on HMI
- Optional emboss / twist only if ordered
Model card — size the copper envelope
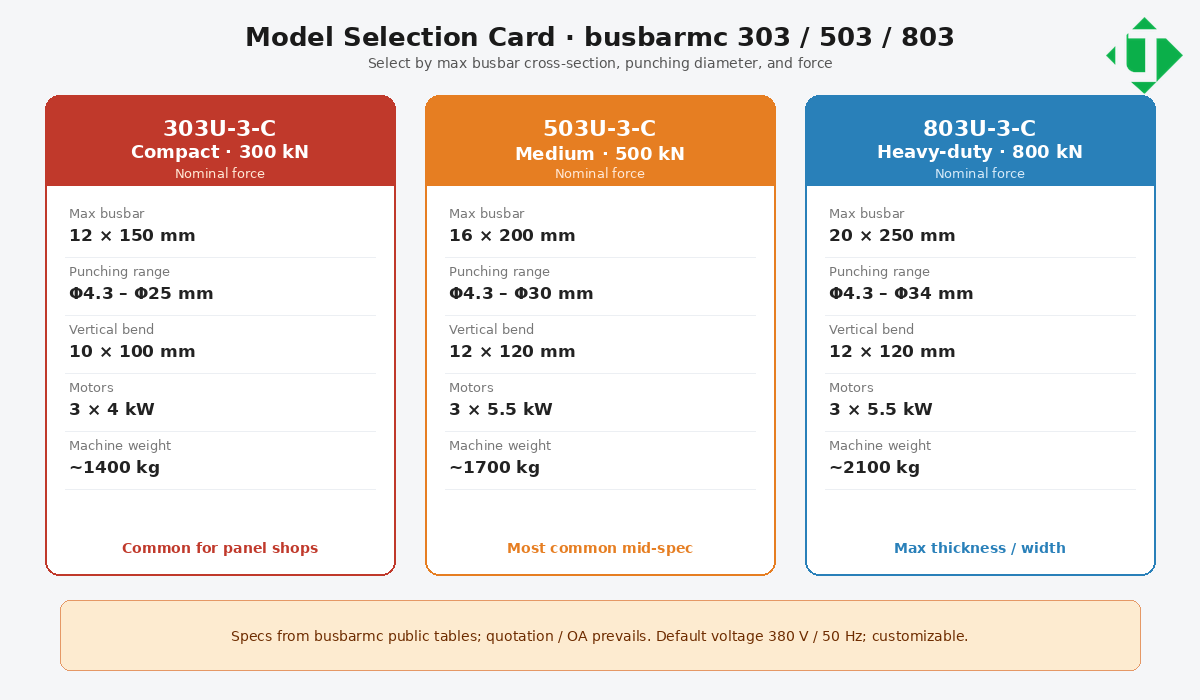
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
| Entity | 303U-3-C | 503U-3-C | 803U-3-C |
|---|---|---|---|
| Nominal force (kN) | 300 | 500 | 800 |
| Punching diameter (mm) | Φ4.3–Φ25 | Φ4.3–Φ30 | Φ4.3–Φ34 |
| Max thickness / width (mm) | 12 / 150 | 16 / 200 | 20 / 250 |
| Max horizontal bend (mm) | 150 / 12 | 200 / 16 | 250 / 20 |
| Max vertical bend size (mm) | 10×100 | 12×120 | 12×120 |
| Motor power | 3×4 kW | 3×5.5 kW | 3×5.5 kW |
Quick cue: 303 ≈ 12×150 / Φ25 · 503 ≈ 16×200 / Φ30 · 803 ≈ 20×250 / Φ34.
How to compare output fairly
Do not compare machines by stroke rate alone. Complete cycle time includes load, setup, tooling, position, punch, move, shear, bend, correct, unload, and inspect. Use the same copper drawing across suppliers; record operators, setup, conforming parts, rejects, and manual interventions.
RFQ package for copper machines
| Send | Used to confirm |
|---|---|
| Grade / temper / max section | Force & handling |
| Drawings (holes, bends, lengths) | Dies & sequence |
| Batch mix & output | 3-in-1 vs line |
| FAT criteria & instruments | Acceptance |
| Voltage / destination | Electrical build |
FAQ
Can one machine cut, punch, and bend copper?
Yes—LTMC three-station models integrate all three. Throughput still depends on staffing and whether pumps run in parallel.
Is nominal force enough to select a copper machine?
No. Verify each station against your hardest hole, shear, and bend family.
What copper thickness can LTMC process?
Public tables: about 12 / 16 / 20 mm max thickness on 303 / 503 / 803—always pair with width and bend limits on the OA.
What should FAT include for copper?
Representative parts: length, hole positions, released bend angles, surface, and consecutive-part variation.
Related technical guides
- Busbar Fabrication Equipment for Nigerian Switchgear, Panel and Busduct Manufacturers
- Three-Station Busbar Machine Guide for Nigerian Panel Builders — 303U-3-C, 503U-3-C and 803U-3-C
- Copper vs Aluminium Busbar Processing for Nigerian Panel Shops — Tooling, Clearance and Springback
- Copper Busbar Punching Guide for 415 V / 50 Hz Nigerian Panel Work — Holes, Dies and Accuracy
Talk to LTMC about a machine for a Nigerian workshop
If you are specifying a punch, cut and bend package for a switchgear, panel or busduct shop in Lagos, Abuja, Port Harcourt or Kano, tell us the copper or aluminium sizes you run, the daily piece count, and whether the machine will sit on a three-phase 415 V / 50 Hz supply. Lighting circuits at 230 V / 50 Hz are not suitable for these machines.
Sea freight is normally arranged to Apapa, Tin Can Island or Lekki Deep Sea Port in Lagos, with Form M and SONCAP documents prepared against the commercial invoice. Leanne will confirm voltage, dies and packing before the machine leaves the factory.
Email [email protected] or WhatsApp +86 13853146766. You can also use the contact form on this site. Public model pages: 3-in-1 busbar machines, 303U-3-C, 503U-3-C, 803U-3-C, plus CNC bending, CNC punching and cutting, and dies and moulds.