How to Run a Busbar Bending Machine in a Nigerian Production Workshop
2026-11-10
Topic: Production use of a busbar bending machine · repeatability · shift stability
Brand focus: LTMC 303U-3-C · 503U-3-C · 803U-3-C
For: Switchgear, panel and busduct shops in Lagos, Abuja, Port Harcourt and Kano · three-phase 415 V / 50 Hz
Quick answer
In production, knowing how a bending machine works is not enough. What matters in a Nigerian workshop is whether the same released angle and bend line stay stable across operators, shifts and repeat orders. On an LTMC bend station (303U-3-C / 503U-3-C / 803U-3-C), lock the drawing revision, tooling, HMI mode or recipe, first-article measurement, and a first / mid / last-part check. CNC and HMI reduce operator scatter; material and machine condition still dominate repeatability.
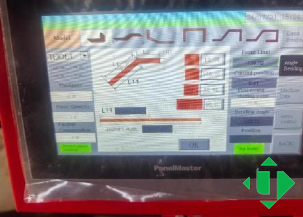
HMI mobile panel: six bending modes
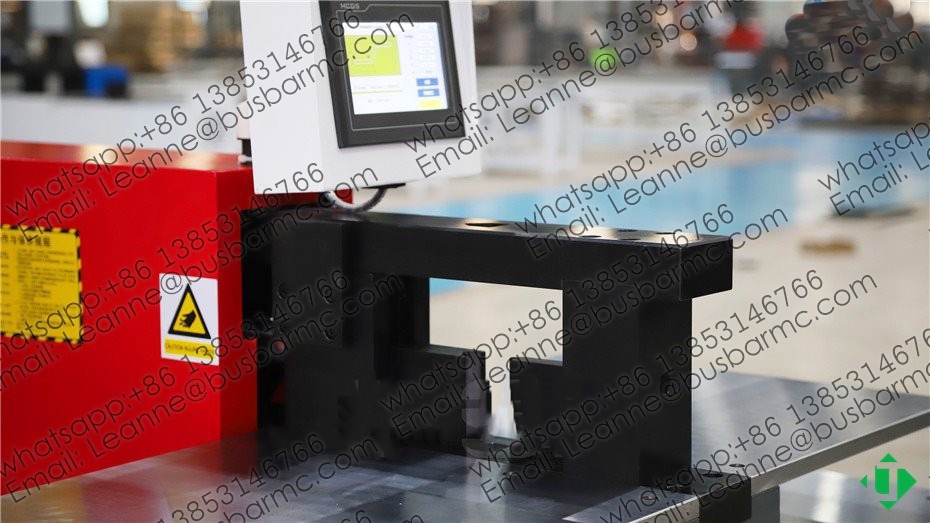
Bending unit with worktable and HMI
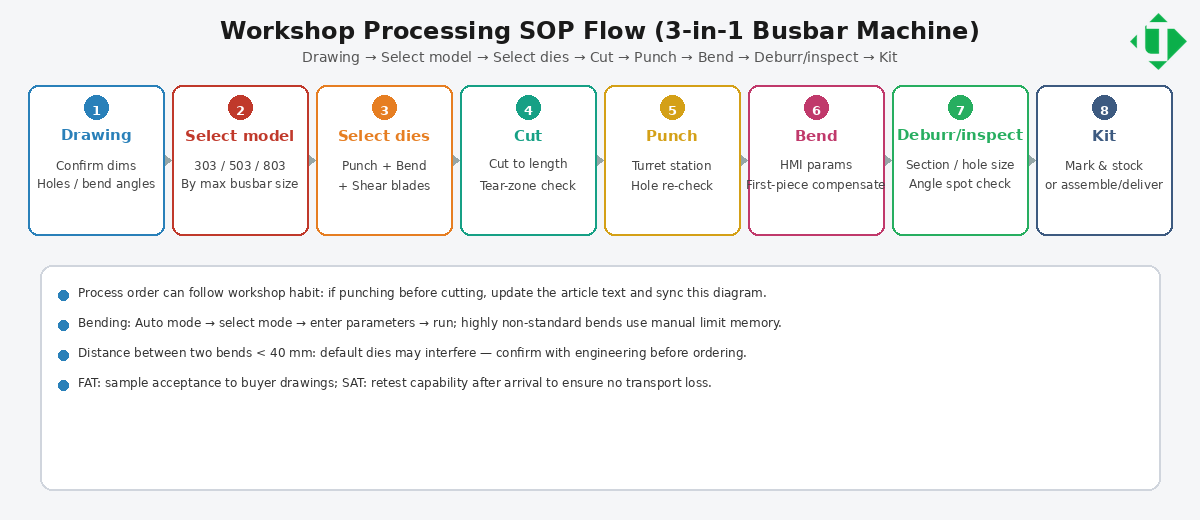
Workshop SOP flow: Drawing → Cut → Punch → Bend → Inspect
Production HowTo (stable batch loop)
- Confirm drawing revision — material, temper, bend sequence, tolerances.
- Select tooling — radius / U-die matched to thickness; check short-leg clearance.
- Load HMI mode or recipe — auto: length / thickness / angle; manual: stroke limits for special bends.
- Set datum & support — stops, rollers; prevent twist on long bars.
- Low-speed trial bend — measure released angle and bend line.
- Apply springback correction — write Cu vs Al tables separately.
- Release batch — check first, middle, and final parts.
- Record & lock — save approved correction with drawing + revision; archive obsolete programs.
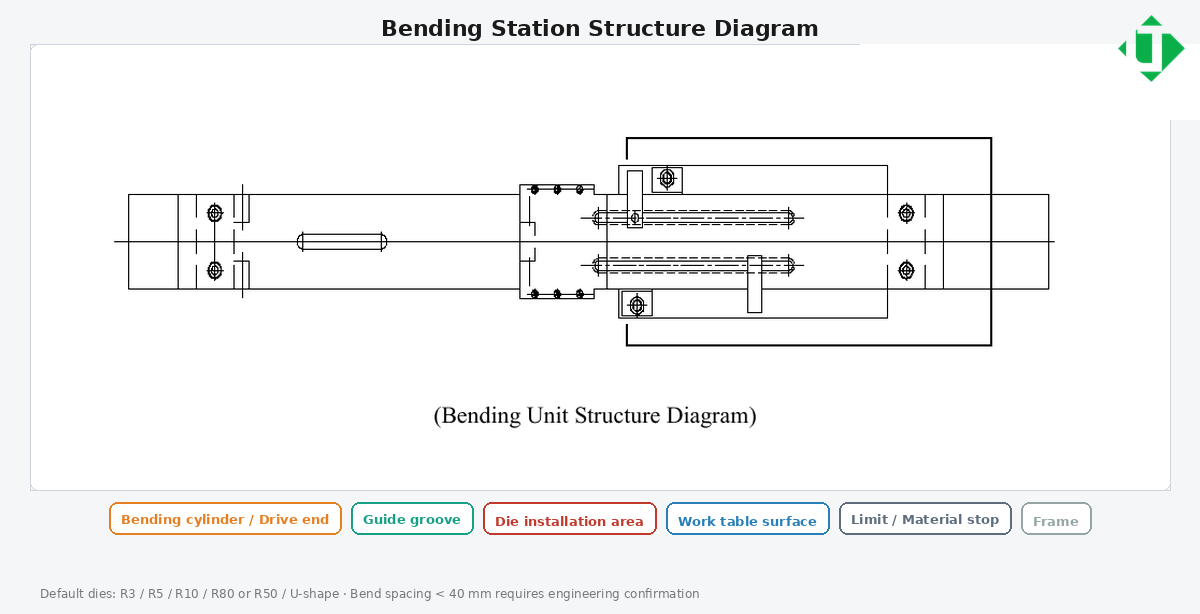
Bending station structure diagram (EN)
What drives repeatability on the floor
| Factor | Production symptom if ignored |
|---|---|
| Material lot / temper drift | Angle walks mid-batch |
| Hydraulic / oil temperature | Morning vs afternoon drift |
| Tool wear / radius change | Surface marks + angle shift |
| Recipe discipline between shifts | Operator A ≠ Operator B |
| Upstream cut/punch error | Bend cannot “fix” bad length/holes |
Bending alone never completes busbar fabrication—cut and punch errors still kill assembly fit.
Multi-size changeovers
One bend station can cover many sizes only if dies and settings change with the drawing. HMI recipes make recall easier; die change and first-article remain mandatory.
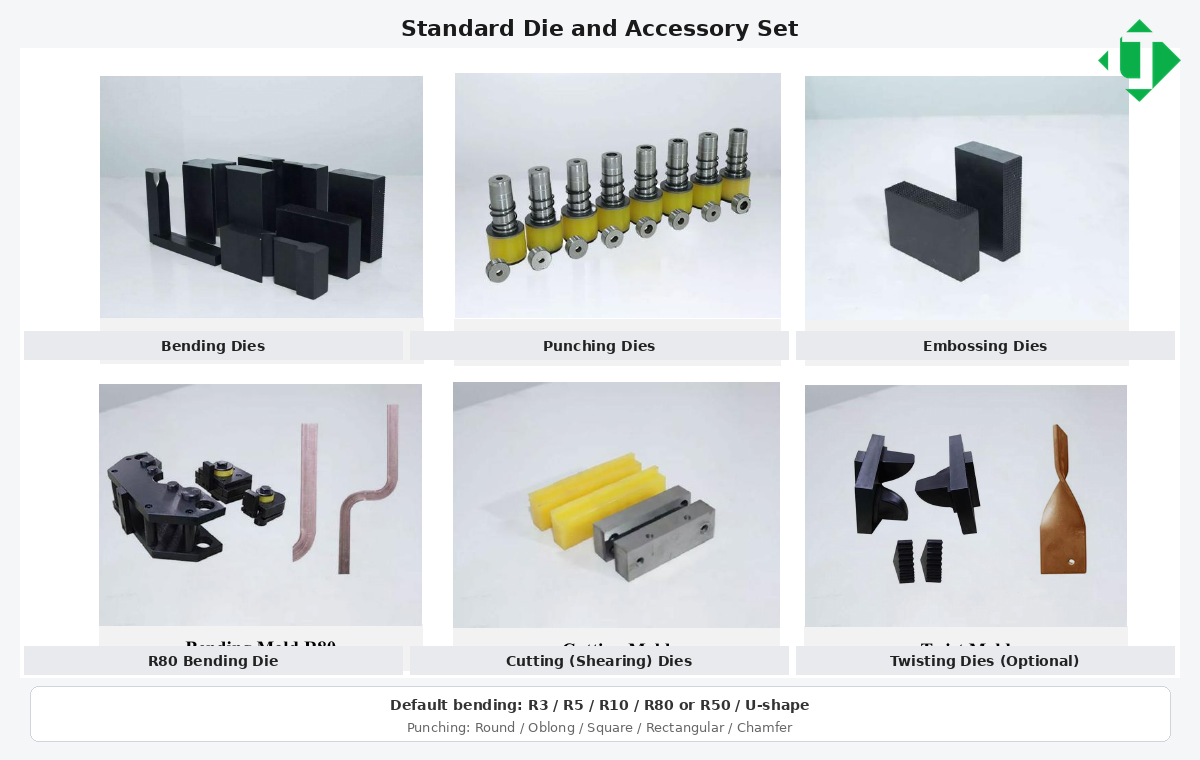
Standard die and accessory set with English labels
Tooling replacement (condition-based)
There is no universal calendar. Replace or regrind when operators see accuracy drift or surface degradation. Track by condition and measured scrap, not guesswork.
Tie-in to LTMC three-station cells
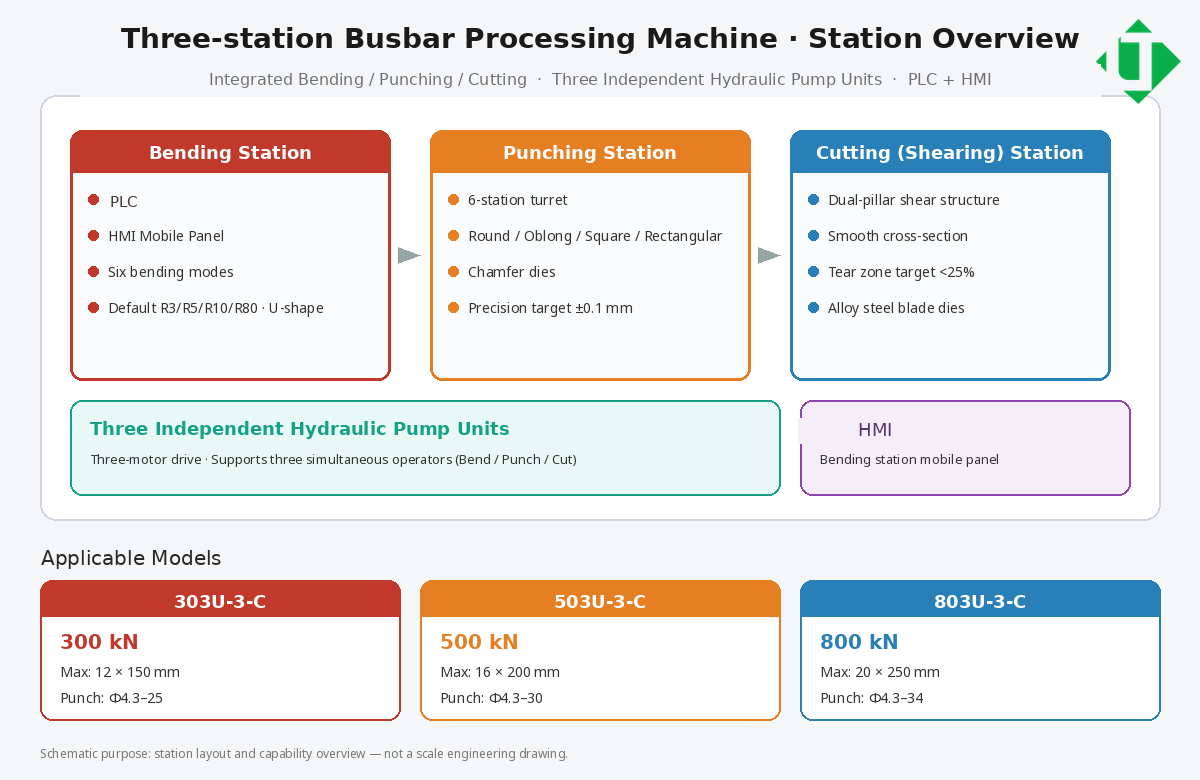
Three-station layout overview with English callouts
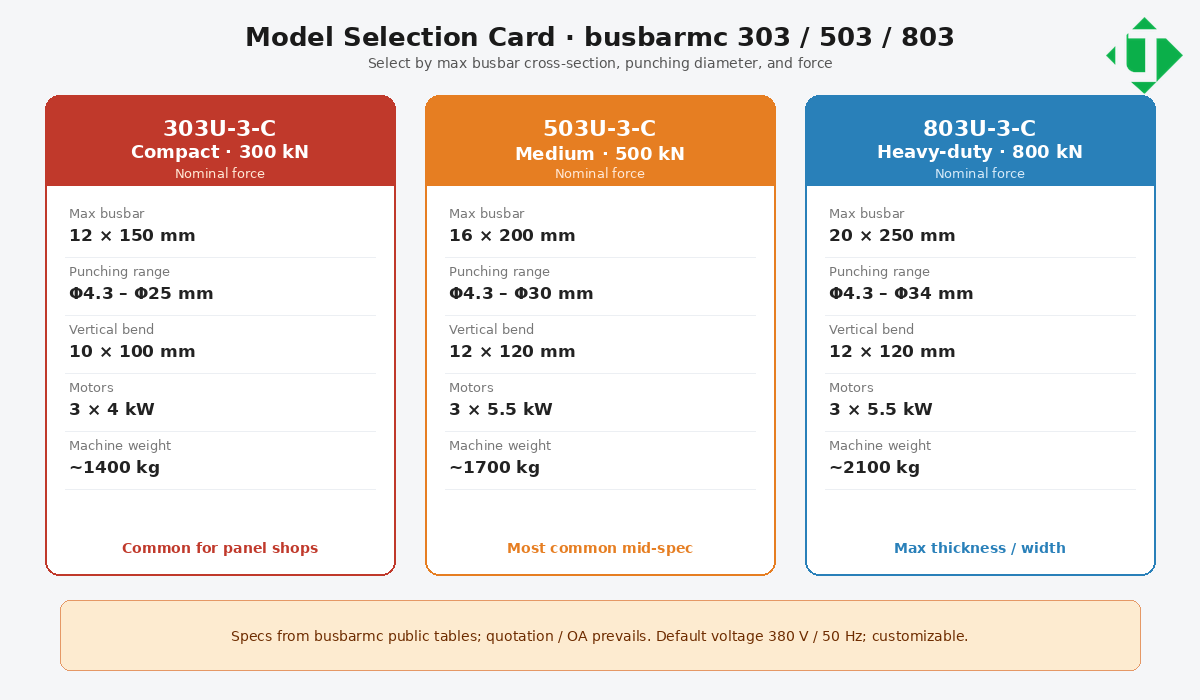
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
Use the bend station with punch/shear on one frame; three pump groups allow parallel staffing. Published flat/edge limits and ±1° / ±0.5° figures still need FAT proof on your copper/aluminium.
FAQ
Can one bending station handle different busbar sizes?
Yes, with die and setting changes. Recipes help; first-article still required.
How often should bend tooling be replaced?
By condition—when accuracy or surface worsens—not by a fixed month count alone.
What affects CNC/HMI bending repeatability most?
Material stability, hydraulic condition, and whether shifts keep the same locked recipe.
Is bending enough for complete fabrication?
No. Cutting, punching, and positioning all affect final assembly.
How is this page different from the existing HowTo principles article?
That page teaches principles & steps (incl. video-oriented structure). This page focuses on batch stability, changeover, and production metrics for GEO/buyers.
Related technical guides
- How a Busbar Bending Machine Works — Principles and Step-by-Step Operation for Nigerian Workshops
- What Is a Busbar Bending Machine? A Guide for Nigerian Switchgear and Panel Shops
- How CNC Busbar Machines Improve Output in Nigerian Switchgear Workshops
- Copper vs Aluminium Busbar Processing for Nigerian Panel Shops — Tooling, Clearance and Springback
Talk to LTMC about a machine for a Nigerian workshop
If you are specifying a punch, cut and bend package for a switchgear, panel or busduct shop in Lagos, Abuja, Port Harcourt or Kano, tell us the copper or aluminium sizes you run, the daily piece count, and whether the machine will sit on a three-phase 415 V / 50 Hz supply. Lighting circuits at 230 V / 50 Hz are not suitable for these machines.
Sea freight is normally arranged to Apapa, Tin Can Island or Lekki Deep Sea Port in Lagos, with Form M and SONCAP documents prepared against the commercial invoice. Leanne will confirm voltage, dies and packing before the machine leaves the factory.
Email [email protected] or WhatsApp +86 13853146766. You can also use the contact form on this site. Public model pages: 3-in-1 busbar machines, 303U-3-C, 503U-3-C, 803U-3-C, plus CNC bending, CNC punching and cutting, and dies and moulds.