Busbar Cutting Machine Guide for Lagos Switchgear and Panel Builders
2026-11-10
Topic: Busbar cutting / shearing · quality metrics · buying tips for Nigerian workshops
Brand focus: LTMC 303U-3-C · 503U-3-C · 803U-3-C
For: Switchgear, panel and busduct shops in Lagos, Abuja, Port Harcourt and Kano · three-phase 415 V / 50 Hz
Quick answer
A busbar cutting (shearing) machine — standalone or as the shear station on a 3-in-1 such as the LTMC 303U-3-C / 503U-3-C / 803U-3-C — should be chosen from material, finished-length tolerance, squareness, burr limit, deformation and production pattern, not catalogue maximum thickness alone. Poor cut edges create rework in punching, bending, assembly and electrical inspection on Nigerian panel and busduct work. Prove quality with documented FAT / continuous cut samples, not a single showpiece.
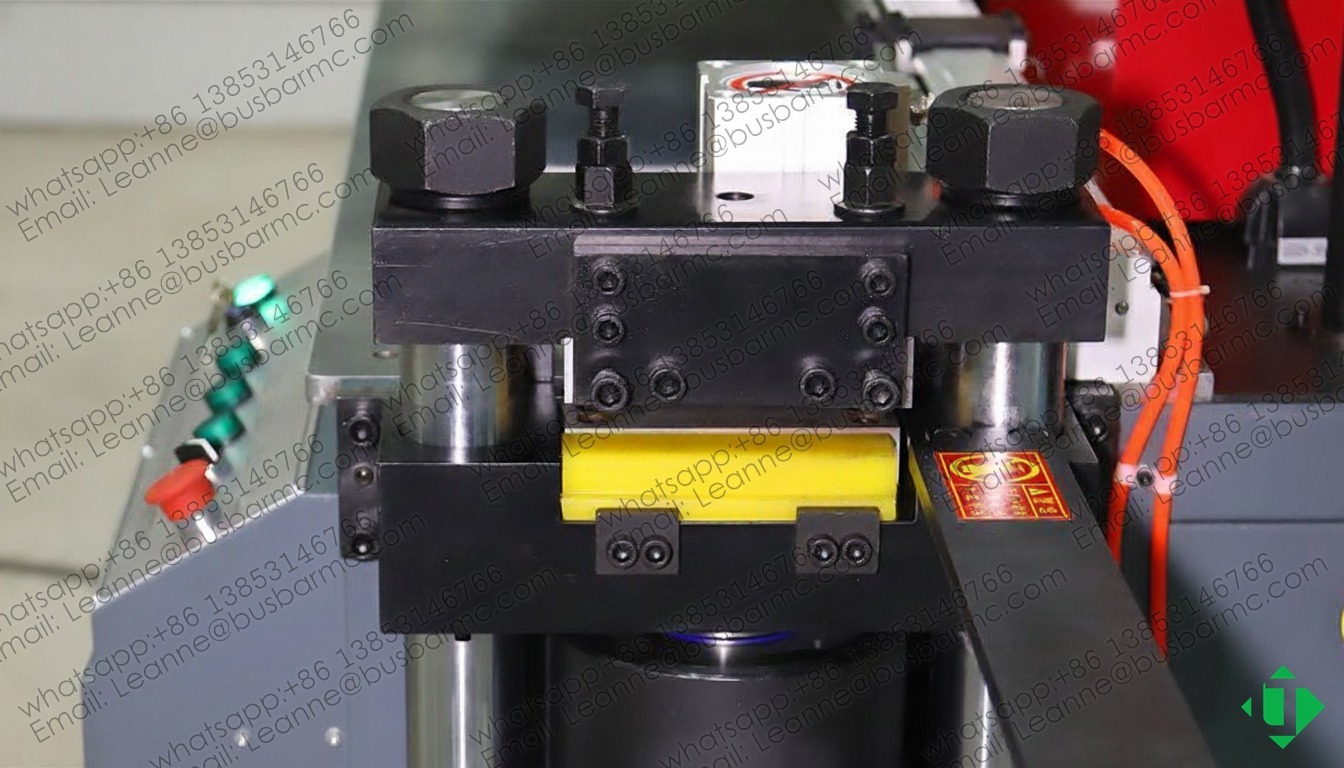
Cutting (shearing) unit close-up
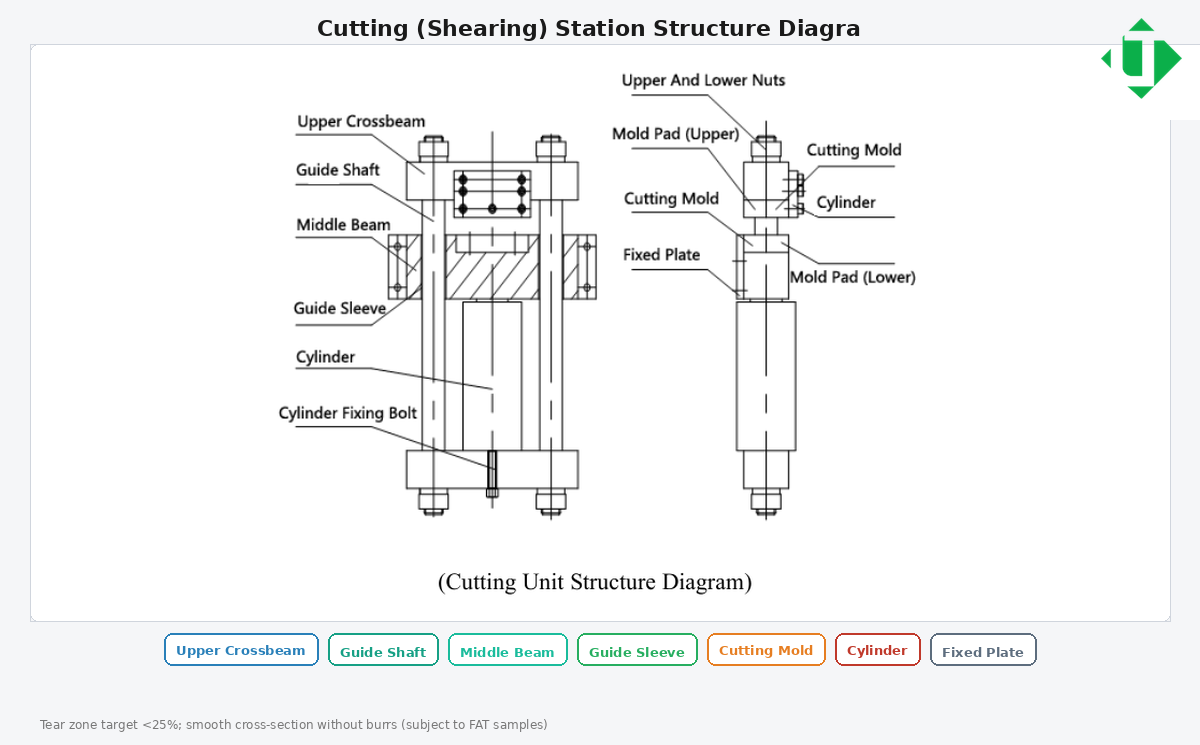
Cutting station structure diagram (EN)
What specifications to confirm before buying
| Specification | Why it matters |
|---|---|
| Material grade (Cu / Al / laminated) | Cutting load and blade choice |
| Temper | Burr, wear, force |
| Width × thickness | Capacity + clearance |
| Raw bar length | Table / roller support |
| Finished length tolerance | Manual stop vs servo / CNC |
| Burr limit | Blade quality + process capability |
| Squareness | Downstream bend / weld / fit |
| Surface / film | Hold-down marks |
| Cycle time | Automation level |
| Positioning method | Manual / servo / CNC |
| Blade spare lead time | Downtime risk |
Cutting methods vs positioning systems
Evaluate how the bar is separated separately from how length is positioned.
Shearing (hydraulic blade)
Common for copper/aluminium busbars: short cycle, limited chips. Edge quality depends on clearance, sharpness, alignment, clamp, and support. Wrong clearance → burrs and local deformation.
Saw cutting
Consider when end profile or material condition makes shearing unsuitable. Expect chips, kerf loss, and often longer cycle time. Compare blade life and secondary finishing—saw is not automatically “higher quality.”
Manual stop vs servo / CNC positioning
| Positioning | Best fit | Watch-out |
|---|---|---|
| Manual stop / scale | Mixed low volume | Operator variation |
| Servo length stop | Recurring lengths | Travel + dead zone |
| CNC program recall | Multi-length kits | Revision control |
Finished-cut results to inspect
Agree before FAT: tolerance, instrument, sample quantity, measure points, inspector, acceptance method.
Inspect: finished length, squareness, max burr height, end deformation, surface damage. For continuous tests, record consecutive parts—not one selected sample—in the FAT pack.
Where cutting sits on a 3-in-1
On LTMC U-3-C machines the shear shares the frame with punch and bend, with independent pump groups so stations can run in parallel when staffed.
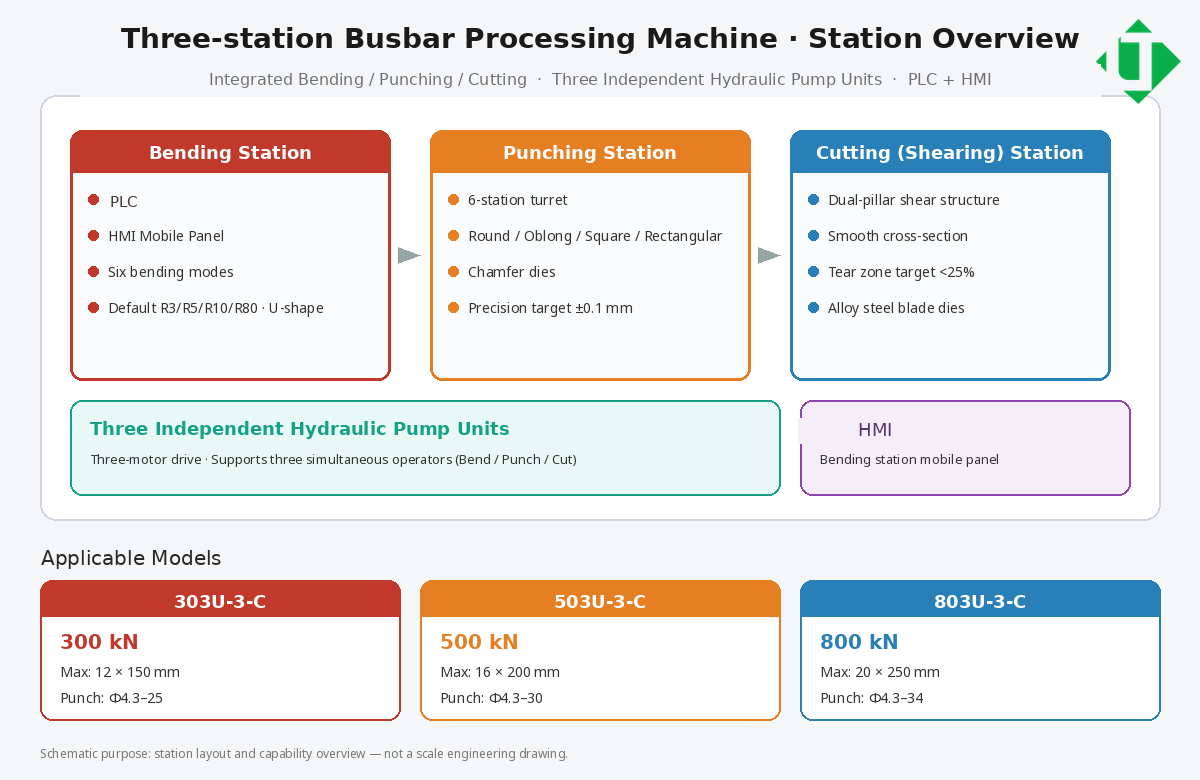
Three-station layout overview with English callouts
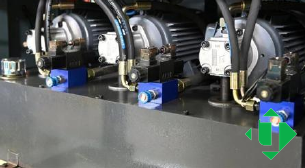
Hydraulic centre: three independent pump units
Published shear envelopes track model class: about 12×150 (303) · 16×200 (503) · 20×250 (803) mm—confirm width wording on OA.
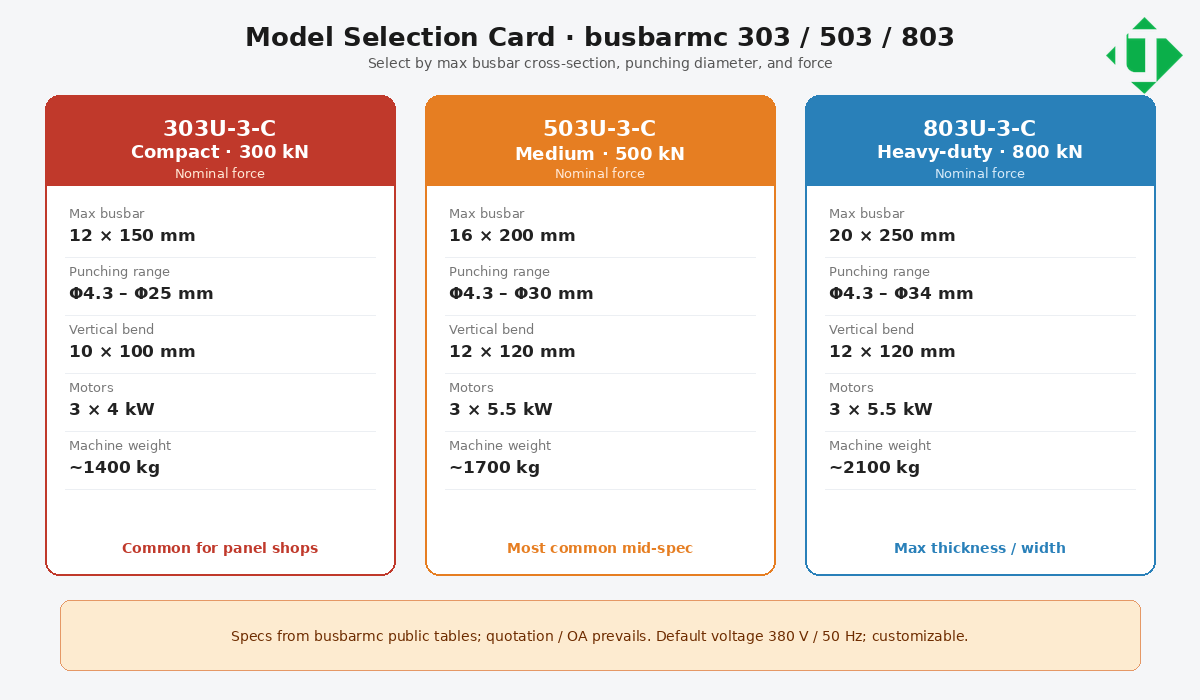
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
Buying tips (decision cues)
- Write acceptance numbers for length / square / burr before RFQ.
- Ask for blade material, clearance guidance, and spare lead time.
- Match positioning to how often lengths repeat.
- If most jobs also punch+bend, prefer a sized 3-in-1 over a lonely shear—unless cutting is the bottleneck.
- Require FAT with your representative section, not only brochure copper.
FAQ
What is a busbar cutting machine?
Equipment that shears or saws copper/aluminium busbars to drawing length with controlled edge quality.
Shear or saw?
Shear for most flat Cu/Al production; saw when the drawing or material rejects shearing. Compare cycle, kerf, chips, and finishing.
Can the shear on a 3-in-1 replace a dedicated cutter?
Often yes for SME mixed work. Choose dedicated cutting when cut hours/day justify a separate station or automatic feed line.
How do I judge cut quality?
Measure length, squareness, burr, deformation, and surface—on multiple consecutive parts under agreed instruments.
What LTMC models cover cutting?
303U-3-C / 503U-3-C / 803U-3-C include hydraulic shear stations sized to the table above.
Related technical guides
- Copper Busbar Punching Guide for 415 V / 50 Hz Nigerian Panel Work — Holes, Dies and Accuracy
- What Is a Busbar Machine? Cutting, Punching and Bending for Nigerian Switchgear Work
- Three-Station Busbar Machine Guide for Nigerian Panel Builders — 303U-3-C, 503U-3-C and 803U-3-C
- How to Choose a Copper Busbar Machine for a Nigerian Panel Shop — Punch, Cut and Bend
Talk to LTMC about a machine for a Nigerian workshop
If you are specifying a punch, cut and bend package for a switchgear, panel or busduct shop in Lagos, Abuja, Port Harcourt or Kano, tell us the copper or aluminium sizes you run, the daily piece count, and whether the machine will sit on a three-phase 415 V / 50 Hz supply. Lighting circuits at 230 V / 50 Hz are not suitable for these machines.
Sea freight is normally arranged to Apapa, Tin Can Island or Lekki Deep Sea Port in Lagos, with Form M and SONCAP documents prepared against the commercial invoice. Leanne will confirm voltage, dies and packing before the machine leaves the factory.
Email [email protected] or WhatsApp +86 13853146766. You can also use the contact form on this site. Public model pages: 3-in-1 busbar machines, 303U-3-C, 503U-3-C, 803U-3-C, plus CNC bending, CNC punching and cutting, and dies and moulds.